 1 / 3
Description
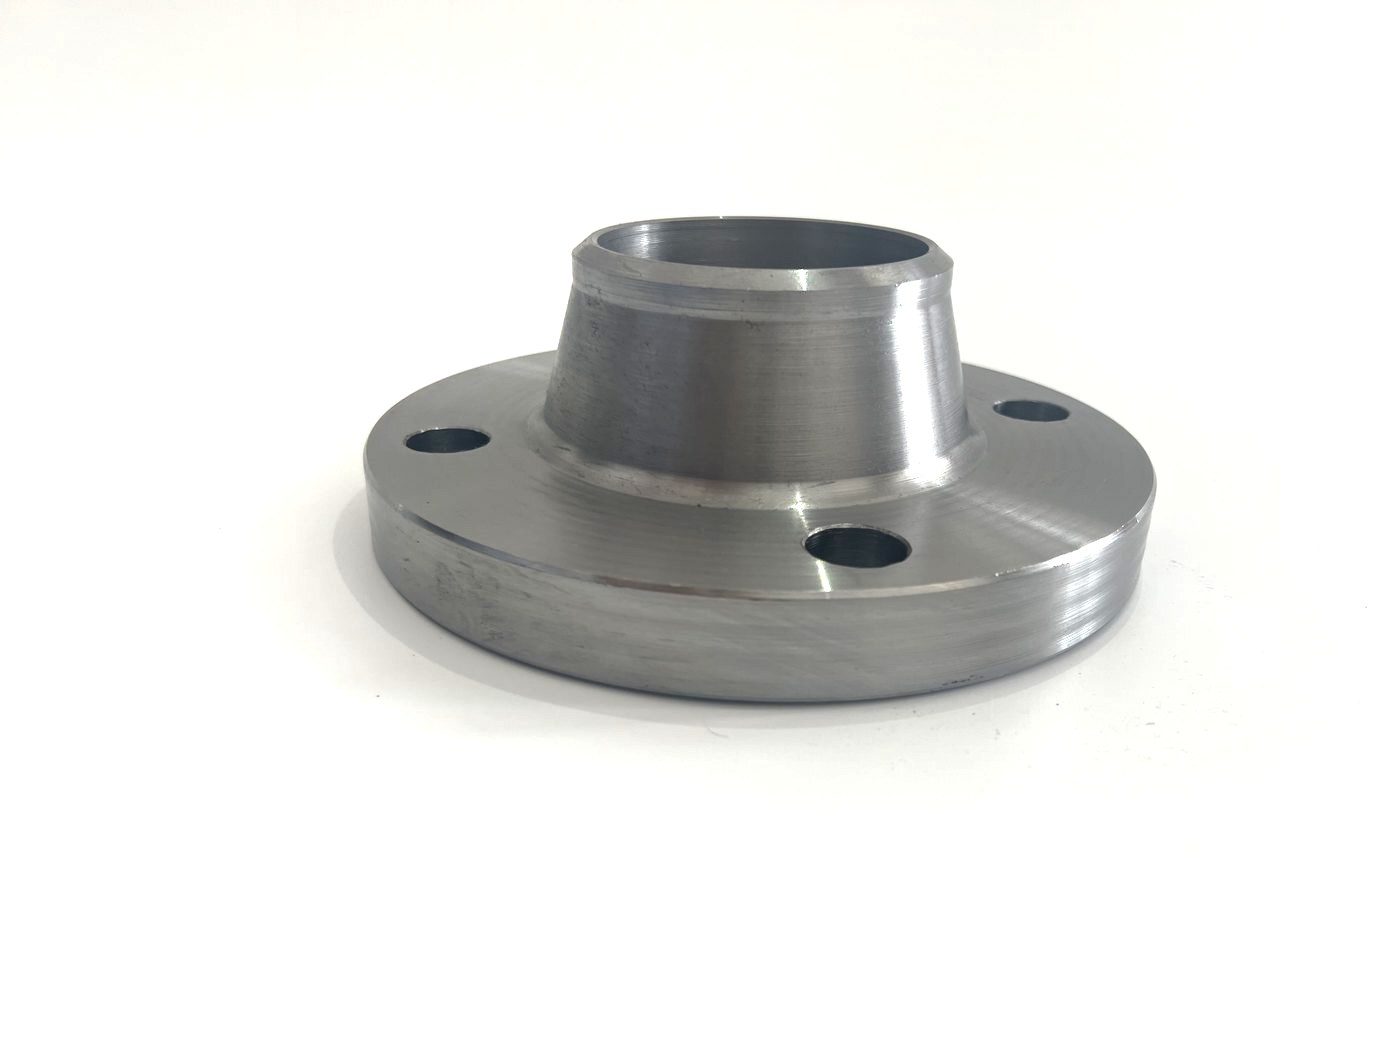
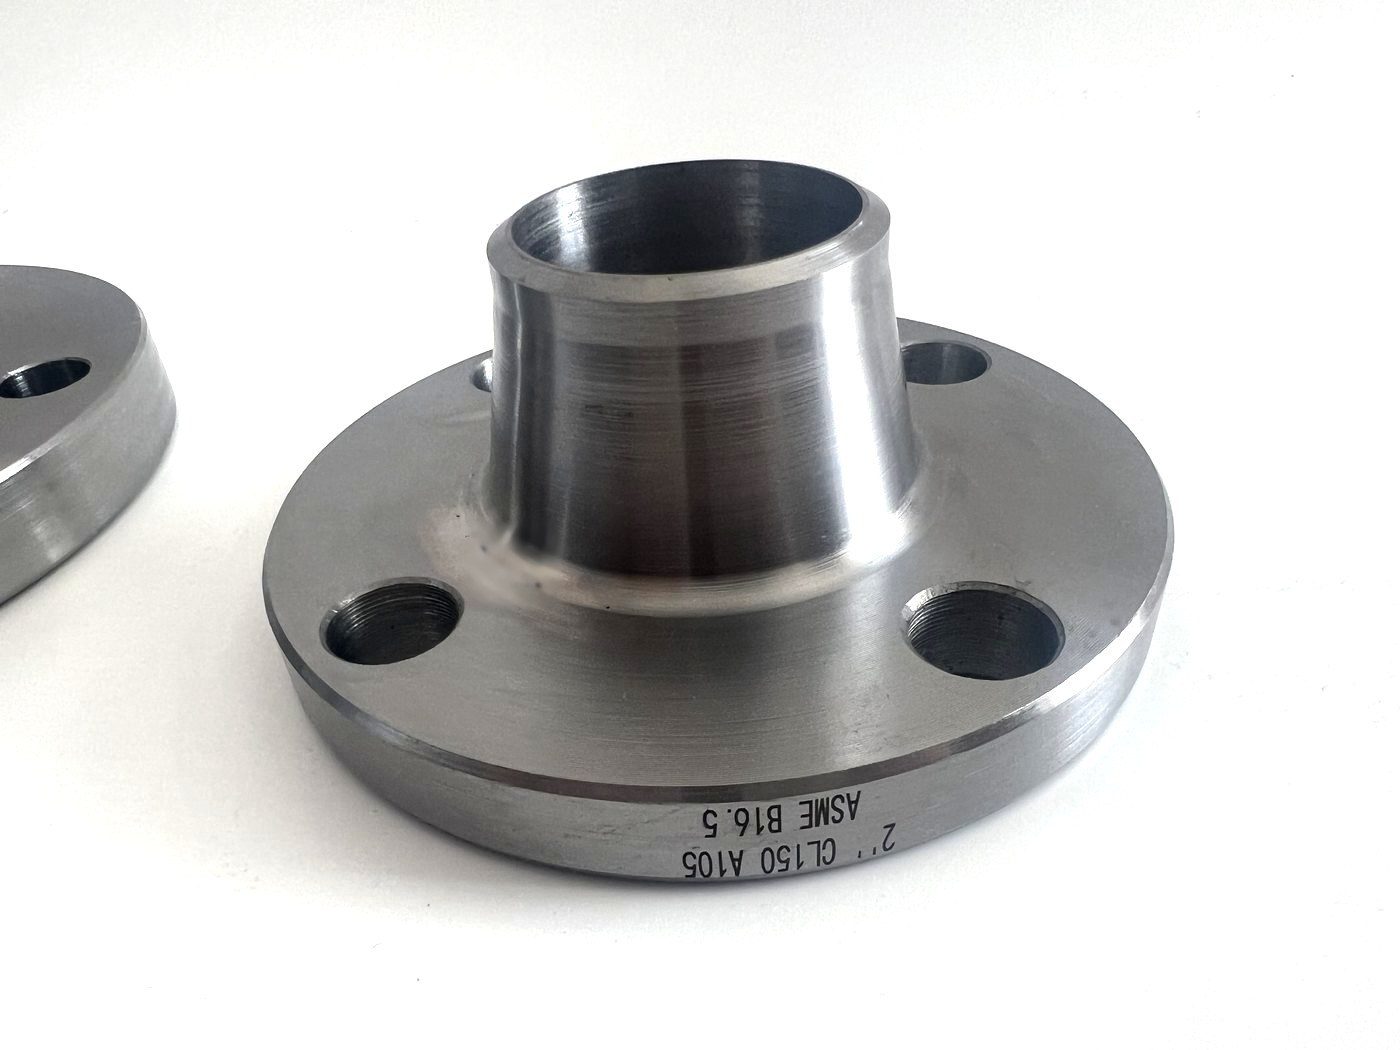
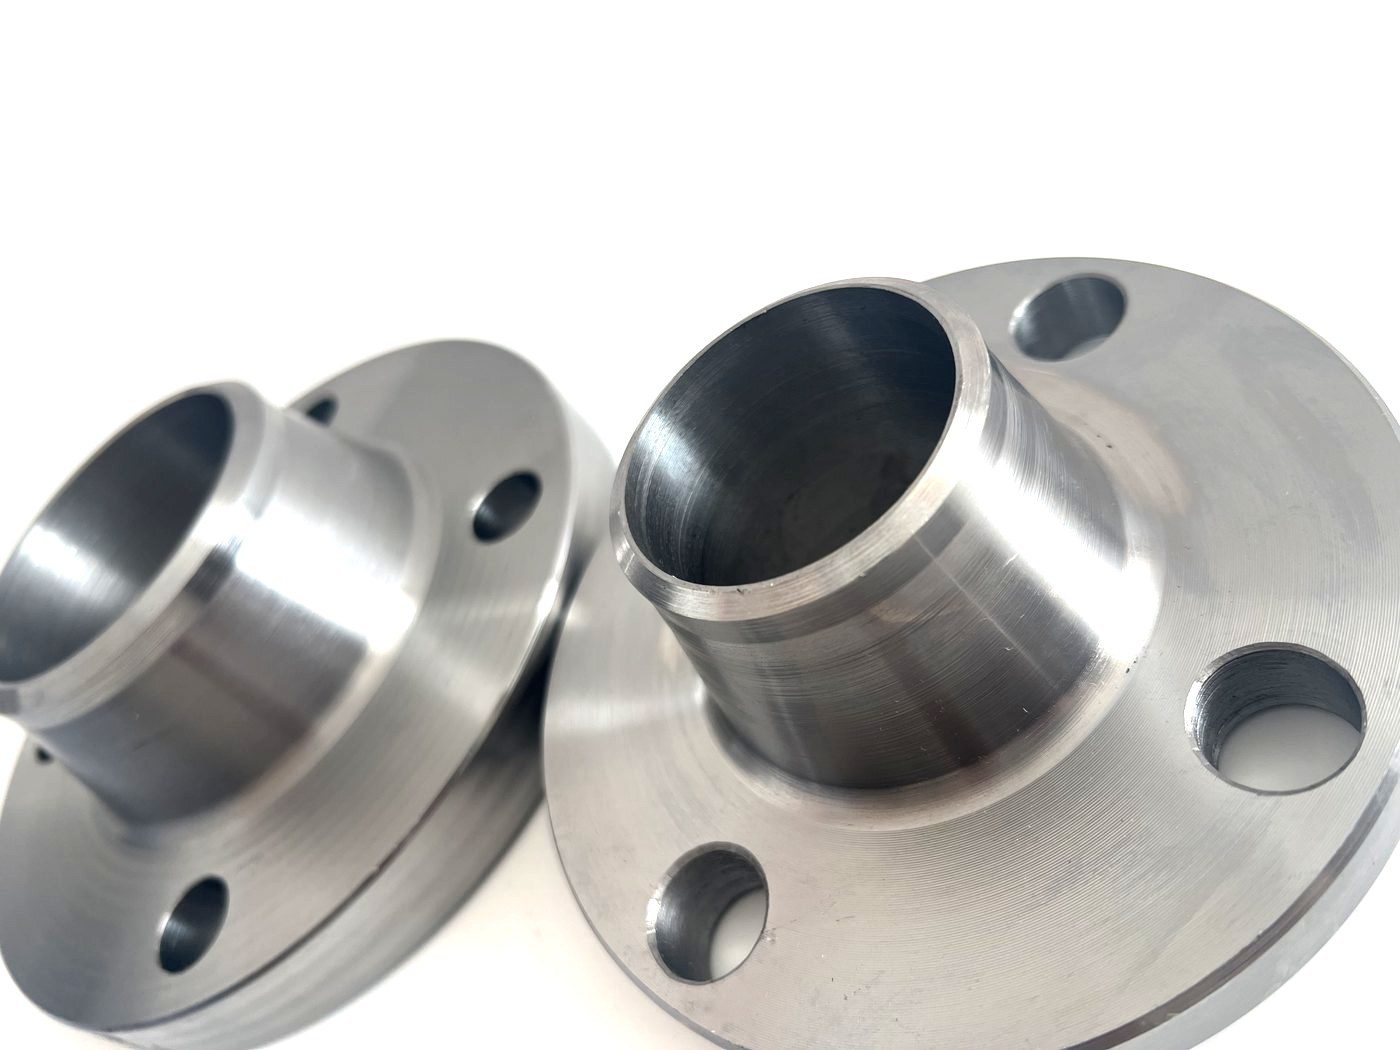
Weld neck flanges (WN) are the standard choice for high-pressure, high-temperature, and critical-service piping systems. The long tapered hub transfers stress from the flange to the pipe, and the butt weld provides full-penetration joint integrity that can be verified by radiographic testing. WN flanges are specified for oil and gas transmission pipelines, refinery process lines, high-pressure steam, high-pressure RO sections of desalination plants, and sour service where failure is not acceptable. We manufacture carbon steel weld neck flanges from our factory in Cangzhou, China's pipe-fitting industrial cluster, covering ASME B16.5 and ASME B16.47 dimensions up to Class 2500. The bore is machined to match your pipe schedule. Each shipment is accompanied by an EN 10204 3.1 Material Test Certificate.
Specifications
| Materials | ASTM A105 (carbon steel) |
| Standards | ASME B16.5 (1/2 inch to 24 inch), ASME B16.47 Series A and Series B (26 inch to 60 inch) |
| Size Range | NPS 1/2 inch to 60 inch |
| Pressure Class | Class 150, Class 300, Class 600, Class 900, Class 1500, Class 2500 (per ASME B16.5 / B16.47) |
| Flange Face Type | RF (Raised Face) — standard for Class 150 to Class 600; RTJ (Ring Type Joint) — standard for Class 900 and above; FF (Flat Face) — on request |
| Bore | Machined to match pipe schedule (SCH 40 / SCH 80 / SCH 160 / XS / XXS / STD). Pipe schedule must be specified at quotation stage. |
| Manufacturing Process | Forged, with tapered hub machined from forgings |
| Surface Treatment | Rust preventive oil + VCI film (standard for sea shipping); hot-dip galvanizing per ASTM A153; cold blackening; clear lacquer |
| MOQ | Negotiable based on specifications and destination port. Standard items can ship from a single pallet; custom orders typically require full container load. |
| Lead Time | Standard items ship within 7-15 days; custom orders and high-pressure classes (Class 900 and above) 25-40 days; shipping time additional depending on destination (typically 30-60 days sea voyage to Middle East ports) |
| HS Code | 7307.91 (carbon steel flanges); GCC Common External Tariff 5% on CIF value for Oman and UAE import |
| Customization | Non-standard sizes, special bore diameters, extended hub lengths, modified thicknesses, and RTJ groove machining are supported. Technical drawings or detailed specifications required for custom orders. |
| Documents | EN 10204 Type 3.1 MTC (standard with every shipment); impact test, hardness test, and NDT reports (RT / UT / MT / PT) on request at quotation stage |
Application Scenarios
Commonly supplied to the following industries and applications:
- Oil and gas gathering and transmission pipelines in Oman, Saudi Arabia, and the UAE — Class 300 to Class 1500 flanges for production, gathering, and export lines
- Oil refinery process units in Sohar, Al Jubail, and Ruwais — Class 300 to Class 900 flanges for hydrocarbon service, hydrotreater and reformer circuits
- High-pressure steam systems in power plants and cogeneration facilities — Class 600 to Class 1500 flanges for main steam and boiler feedwater lines
- Desalination plants along the Gulf coast — Class 600 to Class 900 flanges for high-pressure RO skids and brine rejection sections
- Chemical and petrochemical plants — Class 300 to Class 600 flanges for high-temperature process lines and reactor piping
- Sour gas fields and acid gas handling facilities — Class 600 to Class 1500 flanges supplied to NACE MR0175 / ISO 15156 requirements
- EPC contractors and overseas infrastructure projects — water transmission mains, district cooling networks, airport and industrial park piping, supplied to the project specification and the document package your QA team requires
For low-pressure non-critical utility lines (Class 150, non-cyclic, ambient temperature), slip-on flanges offer a lower-cost alternative.
Samples, Third-Party Inspection and Test Records
Sample pieces can be produced before the batch runs, so that dimensions, bevel profile and fit-up can be checked on your side first. Sample cost and delivery time are advised with the quotation, based on size and material.
Buyer-nominated inspection is supported. SGS, BV, Intertek or your own inspector can witness dimensional checking, marking, coating and container loading at the production site, and we provide the documents and site access needed for the visit. Where a visit is not practical, the same checks can be followed through a live video walkthrough. Third-party inspection fees are normally carried by the buyer.
Non-destructive testing and hydrostatic test records are available on request and can be shipped with the order, together with the EN 10204 3.1 material certificate, the heat number and marking list, dimensional records, packing list and certificate of origin. Tell us at enquiry stage which records your project requires, and they are included in the quotation.
Weld Neck vs Slip-On
| Criterion | Weld Neck (WN) | Slip-On (SO) |
|---|---|---|
| Pressure Class Range | Class 150 - Class 2500 | Class 150 - Class 600 |
| Temperature Limit | Up to ~425°C for ASTM A105 (per ASME B16.5 rating) | Up to ~200°C typical for general service |
| Weld Type | Butt weld (full penetration, double-sided) | Single fillet weld (inside + outside of hub) |
| Weld Strength | Higher (stress distributed through tapered hub) | Lower (stress concentration at pipe end) |
| Bore Match | Machined to pipe schedule, smooth flow path | Slips over pipe OD, step remains at pipe end |
| Inspection | Butt weld radiographic testing (RT) applicable | Fillet weld, visual inspection typically sufficient |
| Cyclic Service | Recommended | Not recommended |
| Sour Service (NACE) | Recommended with NACE MR0175 compliant material | Not recommended |
| Cost (relative) | 100% (baseline) | 60-75% of WN price |
| Typical Applications | Oil & gas, refinery, power plant, high-pressure steam | Water, HVAC, low-pressure utility lines |
| desalination RO, sour service |
Selection Logic
Buyer FAQ
Q1: Weld Neck vs Slip-On — how to choose? Which is specified for refinery process lines?
A1: For refinery process lines, weld neck flanges are the standard specification. The tapered hub and full-penetration butt weld handle the pressure, temperature, and thermal cycling of hydrocarbon service, and the weld can be radiographically tested to ASME B31.3. Slip-on flanges are only used in refineries for low-pressure utility lines such as utility water, instrument air, and drains at Class 150, where service is non-cyclic and non-critical. The dividing line is not pressure alone: cyclic service, flammable fluid, and temperature above 200°C all push the selection to weld neck regardless of pressure class.
Q2: How is the bore of a weld neck flange determined? Do I need to specify pipe schedule?
A2: Yes. The bore of a weld neck flange must be machined to match your pipe inside diameter, which is defined by the pipe schedule (SCH 40, SCH 80, SCH 160, XS, XXS, or STD). Specify the pipe schedule at quotation stage. A mismatched bore leaves a step at the weld joint, which creates turbulence, erosion, and a stress riser at the most critical location in the joint. This is the single most common ordering error for weld neck flanges, and it is not visible from the outside once installed.
Q3: Should I use RTJ or RF facing for high-pressure classes?
A3: RTJ (Ring Type Joint) is the standard facing for Class 900 and above, and is frequently specified for Class 600 in hydrocarbon and high-temperature service. The metal ring gasket seated in the groove provides a pressure-energized seal that performs under pressure and temperature cycling. RF (Raised Face) with a spiral wound gasket is standard for Class 150 to Class 600 in general service. RF and RTJ are not interchangeable — the groove is machined into the flange face and must be specified before production. Your piping class specification normally defines this; if not, share your design pressure and temperature and we will confirm the recommended facing.
Q4: Can weld neck flanges be used in sour service (H2S-containing fluids)?
A4: Yes, weld neck flanges are the required flange type for sour service. Sour gas fields and acid gas handling facilities in the Gulf specify weld neck flanges to NACE MR0175 / ISO 15156, which governs material hardness, heat treatment, and manufacturing controls to prevent sulfide stress cracking. For sour service orders, please state the H2S partial pressure and service temperature at quotation stage so that the material can be supplied and certified to the applicable NACE requirements. Certification documents are provided with the shipment.
Q5: Is radiographic testing (RT) required for weld neck flange welds? What percentage?
A5: The weld itself is performed by your fabricator, so the RT requirement comes from your piping code and fluid service category. Under ASME B31.3, butt welds in normal fluid service typically require 5% random RT, while Category M (toxic) and high-pressure fluid service require 100% RT. The flange itself can be supplied with RT or UT testing of the forging and hub on request, plus MT or PT of the weld prep area. Please state your inspection requirements at quotation stage so testing can be quoted and scheduled into the production lead time.
Q6: Can ASTM A105 weld neck flanges be used for high-pressure steam in power plants?
A6: Yes, within the ASME B16.5 pressure-temperature rating for ASTM A105. The rating is pressure-class dependent, so the allowable temperature drops as the class increases. As a practical guide, A105 is widely used for steam service up to approximately 425°C. Above that range, an alloy material grade is required — please share your design pressure, operating temperature, and steam condition and we will confirm the suitable material. We also recommend stating whether the line sees thermal cycling from start-up and shutdown, because that affects material and inspection selection.
Q7: Why are weld neck flanges mandatory for the high-pressure RO section of desalination plants?
A7: High-pressure RO skids operate at 60-80 bar with continuous pressure cycling from pump start-up and shutdown, and the brine rejection section carries high-chloride water at elevated pressure. Slip-on fillet welds accumulate fatigue damage under this cycling and fail at the pipe end. Weld neck flanges distribute the cyclic stress through the tapered hub into the pipe wall and provide a full-penetration butt weld. Most desalination EPC specifications make weld neck flanges mandatory above Class 300. Material for high-chloride service: standard ASTM A105 for intake and low-salinity sections; for brine and high-chloride exposure, a material upgrade is required — please share your water chemistry and we will confirm the suitable grade.
Q8: Is the hub length of a weld neck flange standard? Can it be extended?
A8: Hub dimensions including overall hub length follow ASME B16.5 and B16.47 and are determined by size and pressure class. Extended hubs, special transition hubs for connecting different wall thicknesses, and long welding neck (LWN) configurations for vessel nozzles are available on request with drawings. Please provide the connecting pipe schedule for both ends if the hub transitions between wall thicknesses, so the bore and the weld prep can be machined correctly.
Q9: Weld neck flanges cost more than slip-on. When is the extra cost justified?
A9: The extra cost is justified whenever the consequence of a joint failure exceeds the price difference, which covers most hydrocarbon, steam, and high-pressure service. A weld neck flange typically costs 25-40% more than an equivalent slip-on flange, but the butt weld is inspectable, the stress path is sound, and the joint survives thermal and pressure cycling. In a refinery or gas plant, a single leak at a utility flange can trigger a shutdown that costs more than the entire flange order. For low-pressure, ambient-temperature, non-cyclic utility lines, slip-on flanges remain the correct economical choice. We can provide side-by-side quotations for both options at your request.
Q10: What is the HS Code and tariff for carbon steel weld neck flanges imported into Oman and the UAE?
A10: Carbon steel weld neck flanges are classified under HS Code 7307.91 (tube or pipe fittings of iron or steel — flanges of iron or steel, other than stainless). GCC Common External Tariff is 5% on CIF value for goods imported into Oman and the UAE. Standard import documentation includes Commercial Invoice, Packing List, Bill of Lading, Certificate of Origin (Form A or applicable FTA), MTC 3.1, and Fumigation Certificate for wooden packaging. Since 2026, electronic Bayan (e-Bayan) declaration is mandatory for Oman customs clearance; UAE importers file through Dubai Customs or the relevant emirate portal. We can provide full export documentation support per your request.
Q11: What sizes and pressure ratings are available for carbon steel weld neck flanges?
A11: NPS 1/2 inch to 60 inch. Class 150, Class 300, Class 600, Class 900, Class 1500 and Class 2500 to ASME B16.5 and B16.47. Sizes and ratings outside this range can be reviewed against your drawing. The exact range confirmed for your order is stated in the quotation.
Q12: How is the wall thickness determined for carbon steel weld neck flanges?
A12: Flange dimensions, including hub and thickness, are fixed by the ASME standard for the size and pressure class you specify. They are not chosen separately. The matching pipe schedule is confirmed at quotation stage.
Q13: What is the lead time for carbon steel weld neck flanges?
A13: Standard sizes in regular material normally take 7-15 days. Non-standard sizes, special materials and custom orders take longer. The exact lead time for this product is given in the specification table on this page and is confirmed in writing with your quotation. Sea freight to the Gulf is additional and depends on the destination port. All lead times are subject to the production schedule at the time of order.
Q14: Is there a minimum order quantity for carbon steel weld neck flanges?
A14: There is no fixed minimum. Standard items can ship from a single pallet, and custom production is normally quoted at full container load. Small trial orders and mixed-size orders are accepted. Send your size list and we will confirm what can be combined in one shipment.
Q15: How are carbon steel weld neck flanges packed and marked?
A15: Flanges and fittings are packed in plywood cases or on plywood pallets with anti-rust treatment, strapped and stretch-wrapped for sea freight. Each piece carries the heat number, and the material, size, standard and pressure class or schedule are marked on the item or on the case label. Shipping marks are printed to your specification, and a fumigation certificate is provided where wooden packaging is used.
Q16: Can you produce carbon steel weld neck flanges to our drawing or to non-standard specifications?
A16: Yes. Send the drawing, material, quantity and the applicable standard, and we will confirm feasibility and quote. Non-standard angles, non-standard schedules, special materials and special dimensions are produced against your drawing. The details we need to quote are listed on our custom service page. The details we need to quote are listed on our custom service page.
Engineer's Note
The following technical guidance reflects the perspective of a senior piping engineer with extensive experience in industrial piping system design.
Weld neck flanges are the default selection for critical service, but the specification details determine whether the joint performs as intended. The following factors should drive your specification:
- Bore and Pipe Schedule Match
- The flange bore must be machined to the pipe inside diameter defined by the pipe schedule
- A bore mismatch leaves a step at the joint: turbulence, erosion, and a stress riser at the worst possible location
- Always state the pipe schedule on the purchase order, not just nominal pipe size
- Pressure Class and Facing Type
- Class 150 to Class 600: RF with spiral wound gasket is standard
- Class 900 and above: RTJ with ring gasket is standard
- Class 600 in hydrocarbon or high-temperature service: RTJ is frequently specified
- RF and RTJ are not interchangeable — the facing must be specified before machining
- Temperature and Material Limit
- ASTM A105 is widely used for steam and hydrocarbon service to approximately 425°C
- Above that range, an alloy material grade is required — share design pressure and temperature for confirmation
- The ASME B16.5 rating is pressure-class dependent: allowable temperature falls as class rises
- Cyclic Service
- Thermal cycling and pressure cycling are the dominant failure driver for flange joints, not static pressure
- Weld neck flanges are the correct selection for any cyclic service regardless of pressure class
- State whether the line sees start-up/shutdown cycling so inspection and material can be matched
- Sour Service (NACE MR0175 / ISO 15156)
- Required for H2S-containing fluids
- Governs material hardness, heat treatment, and manufacturing controls to prevent sulfide stress cracking
- H2S partial pressure and service temperature are required at quotation stage
- Inspection and Testing
- Butt welds are inspectable by RT or UT; fillet welds are not
- ASME B31.3: 5% random RT for normal fluid service, 100% for Category M and high-pressure service
- Forging and hub testing, plus MT or PT of the weld prep, are available on request
- Common Mistakes to Avoid
- Ordering by nominal size without pipe schedule: bore mismatch, invisible after installation
- Specifying RF for Class 900 and above: joint will not seal as designed
- Using ASTM A105 above its temperature limit: creep and graphitization risk
- Omitting NACE requirements on sour service orders: material cannot be certified retroactively
- Assuming slip-on and weld neck are interchangeable to save cost: they are not, in cyclic or flammable service
For project-specific engineering support, please share your service conditions (design pressure, temperature, pipe schedule, fluid composition, cyclic vs static, H2S content) and we will review the specification and provide a written recommendation.
Frequently Asked Questions
Weld Neck vs Slip-On — how to choose? Which is specified for refinery process lines?
For refinery process lines, weld neck flanges are the standard specification. The tapered hub and full-penetration butt weld handle the pressure, temperature, and thermal cycling of hydrocarbon service, and the weld can be radiographically tested to ASME B31.3. Slip-on flanges are only used in refineries for low-pressure utility lines such as utility water, instrument air, and drains at Class 150, where service is non-cyclic and non-critical. The dividing line is not pressure alone: cyclic service, flammable fluid, and temperature above 200°C all push the selection to weld neck regardless of pressure class.
How is the bore of a weld neck flange determined? Do I need to specify pipe schedule?
Yes. The bore of a weld neck flange must be machined to match your pipe inside diameter, which is defined by the pipe schedule (SCH 40, SCH 80, SCH 160, XS, XXS, or STD). Specify the pipe schedule at quotation stage. A mismatched bore leaves a step at the weld joint, which creates turbulence, erosion, and a stress riser at the most critical location in the joint. This is the single most common ordering error for weld neck flanges, and it is not visible from the outside once installed.
Should I use RTJ or RF facing for high-pressure classes?
RTJ (Ring Type Joint) is the standard facing for Class 900 and above, and is frequently specified for Class 600 in hydrocarbon and high-temperature service. The metal ring gasket seated in the groove provides a pressure-energized seal that performs under pressure and temperature cycling. RF (Raised Face) with a spiral wound gasket is standard for Class 150 to Class 600 in general service. RF and RTJ are not interchangeable — the groove is machined into the flange face and must be specified before production. Your piping class specification normally defines this; if not, share your design pressure and temperature and we will confirm the recommended facing.
Can weld neck flanges be used in sour service (H2S-containing fluids)?
Yes, weld neck flanges are the required flange type for sour service. Sour gas fields and acid gas handling facilities in the Gulf specify weld neck flanges to NACE MR0175 / ISO 15156, which governs material hardness, heat treatment, and manufacturing controls to prevent sulfide stress cracking. For sour service orders, please state the H2S partial pressure and service temperature at quotation stage so that the material can be supplied and certified to the applicable NACE requirements. Certification documents are provided with the shipment.
Is radiographic testing (RT) required for weld neck flange welds? What percentage?
The weld itself is performed by your fabricator, so the RT requirement comes from your piping code and fluid service category. Under ASME B31.3, butt welds in normal fluid service typically require 5% random RT, while Category M (toxic) and high-pressure fluid service require 100% RT. The flange itself can be supplied with RT or UT testing of the forging and hub on request, plus MT or PT of the weld prep area. Please state your inspection requirements at quotation stage so testing can be quoted and scheduled into the production lead time.
Can ASTM A105 weld neck flanges be used for high-pressure steam in power plants?
Yes, within the ASME B16.5 pressure-temperature rating for ASTM A105. The rating is pressure-class dependent, so the allowable temperature drops as the class increases. As a practical guide, A105 is widely used for steam service up to approximately 425°C. Above that range, an alloy material grade is required — please share your design pressure, operating temperature, and steam condition and we will confirm the suitable material. We also recommend stating whether the line sees thermal cycling from start-up and shutdown, because that affects material and inspection selection.
Why are weld neck flanges mandatory for the high-pressure RO section of desalination plants?
High-pressure RO skids operate at 60-80 bar with continuous pressure cycling from pump start-up and shutdown, and the brine rejection section carries high-chloride water at elevated pressure. Slip-on fillet welds accumulate fatigue damage under this cycling and fail at the pipe end. Weld neck flanges distribute the cyclic stress through the tapered hub into the pipe wall and provide a full-penetration butt weld. Most desalination EPC specifications make weld neck flanges mandatory above Class 300. Material for high-chloride service: standard ASTM A105 for intake and low-salinity sections; for brine and high-chloride exposure, a material upgrade is required — please share your water chemistry and we will confirm the suitable grade.
Is the hub length of a weld neck flange standard? Can it be extended?
Hub dimensions including overall hub length follow ASME B16.5 and B16.47 and are determined by size and pressure class. Extended hubs, special transition hubs for connecting different wall thicknesses, and long welding neck (LWN) configurations for vessel nozzles are available on request with drawings. Please provide the connecting pipe schedule for both ends if the hub transitions between wall thicknesses, so the bore and the weld prep can be machined correctly.
Weld neck flanges cost more than slip-on. When is the extra cost justified?
The extra cost is justified whenever the consequence of a joint failure exceeds the price difference, which covers most hydrocarbon, steam, and high-pressure service. A weld neck flange typically costs 25-40% more than an equivalent slip-on flange, but the butt weld is inspectable, the stress path is sound, and the joint survives thermal and pressure cycling. In a refinery or gas plant, a single leak at a utility flange can trigger a shutdown that costs more than the entire flange order. For low-pressure, ambient-temperature, non-cyclic utility lines, slip-on flanges remain the correct economical choice. We can provide side-by-side quotations for both options at your request.
What is the HS Code and tariff for carbon steel weld neck flanges imported into Oman and the UAE?
Carbon steel weld neck flanges are classified under HS Code 7307.91 (tube or pipe fittings of iron or steel — flanges of iron or steel, other than stainless). GCC Common External Tariff is 5% on CIF value for goods imported into Oman and the UAE. Standard import documentation includes Commercial Invoice, Packing List, Bill of Lading, Certificate of Origin (Form A or applicable FTA), MTC 3.1, and Fumigation Certificate for wooden packaging. Since 2026, electronic Bayan (e-Bayan) declaration is mandatory for Oman customs clearance; UAE importers file through Dubai Customs or the relevant emirate portal. We can provide full export documentation support per your request.
What sizes and pressure ratings are available for carbon steel weld neck flanges?
NPS 1/2 inch to 60 inch. Class 150, Class 300, Class 600, Class 900, Class 1500 and Class 2500 to ASME B16.5 and B16.47. Sizes and ratings outside this range can be reviewed against your drawing. The exact range confirmed for your order is stated in the quotation.
How is the wall thickness determined for carbon steel weld neck flanges?
Flange dimensions, including hub and thickness, are fixed by the ASME standard for the size and pressure class you specify. They are not chosen separately. The matching pipe schedule is confirmed at quotation stage.
What is the lead time for carbon steel weld neck flanges?
Standard sizes in regular material normally take 7-15 days. Non-standard sizes, special materials and custom orders take longer. The exact lead time for this product is given in the specification table on this page and is confirmed in writing with your quotation. Sea freight to the Gulf is additional and depends on the destination port. All lead times are subject to the production schedule at the time of order.
Is there a minimum order quantity for carbon steel weld neck flanges?
There is no fixed minimum. Standard items can ship from a single pallet, and custom production is normally quoted at full container load. Small trial orders and mixed-size orders are accepted. Send your size list and we will confirm what can be combined in one shipment.
How are carbon steel weld neck flanges packed and marked?
Flanges and fittings are packed in plywood cases or on plywood pallets with anti-rust treatment, strapped and stretch-wrapped for sea freight. Each piece carries the heat number, and the material, size, standard and pressure class or schedule are marked on the item or on the case label. Shipping marks are printed to your specification, and a fumigation certificate is provided where wooden packaging is used.
Can you produce carbon steel weld neck flanges to our drawing or to non-standard specifications?
Yes. Send the drawing, material, quantity and the applicable standard, and we will confirm feasibility and quote. Non-standard angles, non-standard schedules, special materials and special dimensions are produced against your drawing. The details we need to quote are listed on our custom service page.
Related products
- carbon steel slip-on flanges
- carbon steel blind flanges
- stainless steel weld neck flanges
- EN 10204 3.1 material certificate